| Softening point | APAO grades commonly span approximately 80–150°C, depending on polymer structure and grade. | Indicates the temperature at which the material softens under a specified test; it helps assess heat resistance and handling behavior. | Compare values measured using the same method, such as ASTM E28. Confirm that the finished adhesive meets the product’s service-temperature requirements. |
| Melt viscosity | Highly grade- and temperature-dependent; compare measured values at the intended application temperature. Results are commonly reported in mPa·s (cP). | Viscosity affects pumping, coating, sprayability, wetting, and the ability to apply a consistent adhesive layer. | Request viscosity data at a stated temperature and test method, such as ASTM D3236. Check performance on the actual equipment and application line. |
| Open time | Varies with formulation, application temperature, adhesive add-ons, substrate, and ambient conditions; there is no single universal APAO value. | Defines the practical interval in which the adhesive can form a bond after application. | Measure under representative production conditions. Choose an open time that allows assembly while avoiding an unnecessarily long setting cycle. |
| Set time | Application- and substrate-dependent; assess using the intended bond geometry and production conditions. | Influences how quickly a bonded assembly can be handled or moved after joining. | Run trials at the planned line speed, substrate temperature, and adhesive coat weight; verify bond strength after cooling. |
| Density | Many unfilled polyolefin-based APAO materials are approximately 0.85–0.90 g/cm³; the exact value depends on grade and additives. | Can help with material comparison, volume-to-mass calculations, and process or packaging estimates. | Use the supplier’s measured value for the specific grade and confirm whether the figure applies to the neat polymer or a formulated adhesive. |
| Thermal stability | Evaluate by observing viscosity, color, odor, and residue after exposure to the intended melt temperature and residence time. | Prolonged heat exposure can contribute to viscosity drift, discoloration, odor, or deposits that affect production consistency. | Test at the actual operating temperature and expected tank residence time. Follow the grade’s recommended processing temperature and handling guidance. |
| Substrate adhesion | Performance depends on substrate type, surface condition, formulation, temperature, and bond design. | A suitable APAO grade must wet and bond the materials used in the end application, including relevant polyolefin surfaces. | Test the actual substrates, including coatings or recycled content where applicable. Assess peel or other application-relevant bond performance. |
| Flexibility and low-temperature behavior | Grade-dependent; evaluate on the finished adhesive bond over the intended use-temperature range. | These properties affect whether a bond remains functional during bending, impact, or cold storage and use. | Condition bonded samples at the relevant temperatures and test for cracking, loss of adhesion, or bond failure. |
| Compatibility with formulation ingredients | Compatibility varies with tackifiers, waxes, oils, antioxidants, and other additives. | Incompatibility can cause phase separation, haze, unstable viscosity, or inconsistent adhesive performance. | Check blend uniformity and stability after heating and storage; assess the complete formulation rather than the polymer alone. |
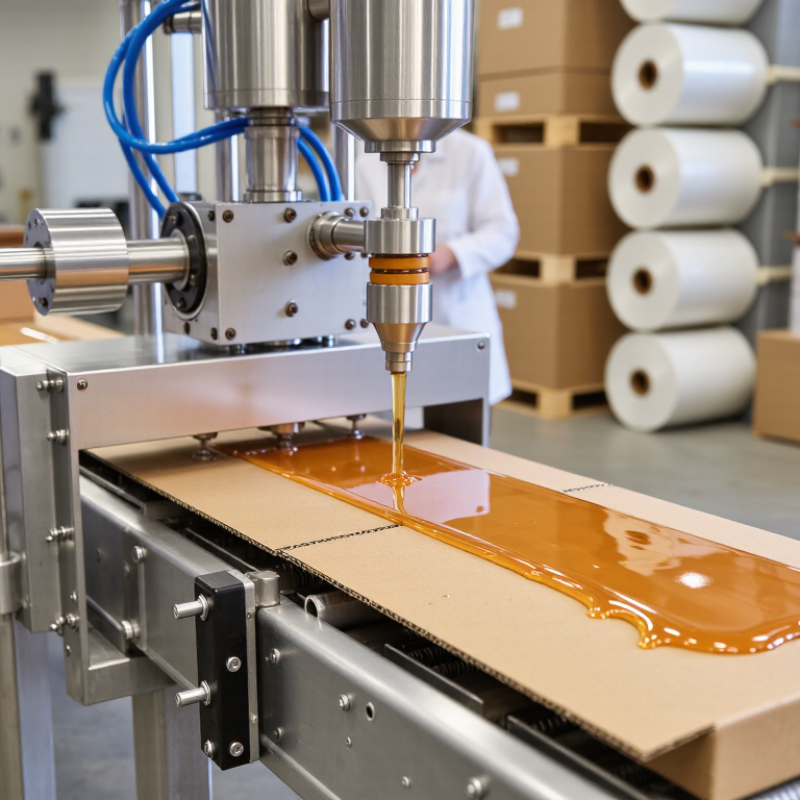
| Application fit | Selection depends on the required coating method, line speed, coat weight, and equipment temperature limits. | A grade that works in one application may not provide the right flow, open time, or bond formation in another. | Confirm suitability for the intended process—such as coating, slot application, or spray—and conduct a production-representative trial. |